Skip to content
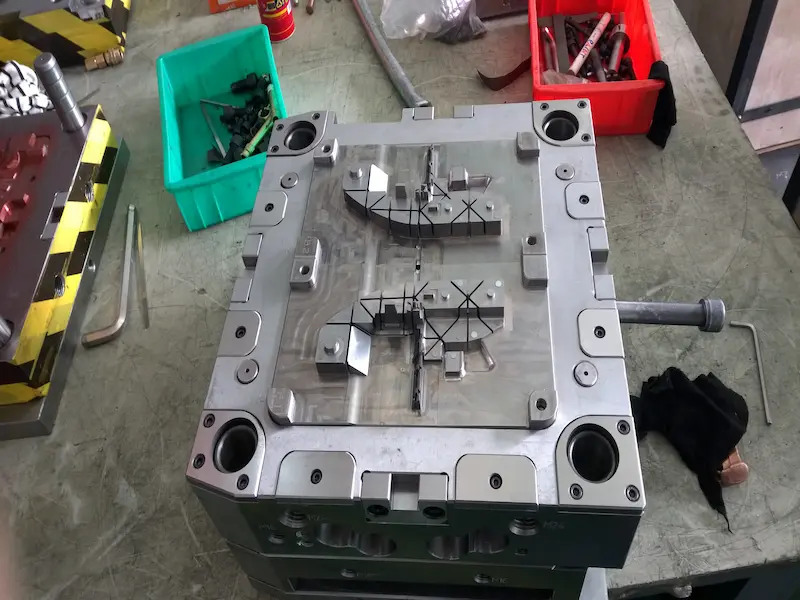
Wire EDM is widely used for machining mold inserts, punches, dies, precision profiles, narrow slots, and hardened tool steels. Because the process does not rely on conventional cutting force, it is particularly useful for complex and high-precision components.
However, unstable machining conditions can result in wire breakage, poor surface finish, dimensional deviation, taper, wire marks, and low machining efficiency. Understanding the causes of these problems helps improve both accuracy and process stability.
1. Frequent Wire Breakage
Wire breakage is one of the most common Wire EDM problems. Possible causes include excessive discharge energy, insufficient flushing, incorrect wire tension, unstable wire feed, poor workpiece conductivity, or contamination in the dielectric system.
The first step is to check whether flushing is stable around the cutting area. Wire tension and feed speed should then be verified together with the selected machining parameters.
For thick workpieces or difficult flushing conditions, overly aggressive cutting parameters can generate excessive heat and debris in the cutting gap.
2. Unstable Discharge
A stable electrical discharge gap is essential for consistent Wire EDM machining. If chips and particles remain concentrated in the gap, short circuits and unstable discharge may occur.
Typical causes include insufficient dielectric flow, blocked flushing nozzles, unsuitable nozzle position, dirty dielectric fluid, or inappropriate machining parameters.
Improving debris removal and adjusting pulse conditions normally provides better stability than simply increasing machining power.
3. Poor Surface Finish
A rough or uneven surface can result from excessive discharge energy, unstable flushing, worn wire, incorrect finishing parameters, or insufficient skim cutting.
Precision mold components often require a rough cut followed by one or more finishing passes. Each finishing pass uses lower discharge energy and a suitable offset to gradually improve surface quality and dimensional accuracy.
4. Dimensional Deviation
Wire EDM dimensions are influenced by wire diameter, discharge gap, offset compensation, machine calibration, thermal conditions, and the number of finishing passes.
If the final size is consistently too large or too small, the programmed offset should be checked together with the actual wire condition and machining technology used.
Critical mold components should be inspected after machining rather than relying only on programmed dimensions.
5. Taper or Vertical Accuracy Problems
A part may measure correctly at one height but show deviation between the upper and lower surfaces. This can be caused by wire deflection, incorrect upper and lower guide alignment, unsuitable tension, poor flushing, or excessive cutting speed.
Thicker workpieces are more sensitive to these conditions. Reducing machining load and improving wire stability can help maintain vertical accuracy.
6. Corner Accuracy Problems
Sharp internal and external corners are difficult because the wire changes direction while continuing to discharge material. If the machine travels through a corner too quickly, wire lag may reduce corner accuracy.
Modern Wire EDM systems use corner control strategies that automatically adjust machining conditions, but suitable parameters and finishing passes are still important for precision mold components.
7. Visible Wire Marks
Vertical lines or other wire marks may appear when machining conditions fluctuate during cutting. Possible causes include vibration, unstable wire tension, contamination, poor guides, unstable discharge, or inconsistent flushing.
Checking the wire transport system and machine maintenance condition is therefore important before changing only the electrical parameters.
8. Low Machining Efficiency
Slow Wire EDM machining is not always solved by increasing discharge power. Excessive energy can actually cause more wire breaks and unstable cutting.
Efficiency should be optimized by balancing discharge parameters, wire speed, wire tension, flushing, workpiece thickness, material, and required surface quality.
Practical Wire EDM Process Control
Before production machining, the operator should confirm machine condition, dielectric cleanliness, wire condition, guides, flushing nozzles, electrical contact, and workpiece setup.
For precision mold components, rough machining and finishing passes should be planned according to the required tolerance and surface finish. Dimensional inspection should also be included in the machining process rather than performed only after all work is complete.
Stable Wire EDM machining comes from controlling the complete process. Correct parameters are important, but machine condition, flushing, wire control, setup, and inspection are equally important for obtaining consistent precision components.